Chapter 13
Infection control and choosing materials
The finished object, its cleaning route, and claims you cannot support
Human Biology for the Medical Maker
Why this chapter exists
- Handled, carried, set down, cleaned by someone else, stored, reused, dropped, repaired
- Every stage is a design input — decided in CAD, on the pattern, at the bench
- A cavity you cannot reach; a seam that traps fluid; a surface the wipe cannot wet
"It's PLA, that's food safe." "It's surgical stainless." "It's medical-grade silicone." These sound like evidence and are not.
Microbiology, in the amount you need
Agents, biofilm, and the chain of infection
The agents
| Agent | Why it matters to an object |
|---|
| Bacteria | Multiply on surfaces with moisture and nutrients; some form biofilm |
| Bacterial spores | Survive many disinfectants; sterilisation is defined by killing them |
| Viruses | Enveloped ones are easier to inactivate; non-enveloped, like norovirus, are tougher |
| Fungi | Grow in damp, porous, absorbent materials |
| Prions | Extraordinarily resistant — a specialist domain |
Biofilm, and why surface finish is not fussiness
- Bacteria attached to a surface secrete a protective matrix
- Far more resistant to disinfectants and wiping
- Forms in crevices, threads, lumens, scratches, porous surfaces
- And in the gaps between press-fitted parts
A scratched or porous surface is not just harder to clean. It provides protected habitat.
The chain of infection
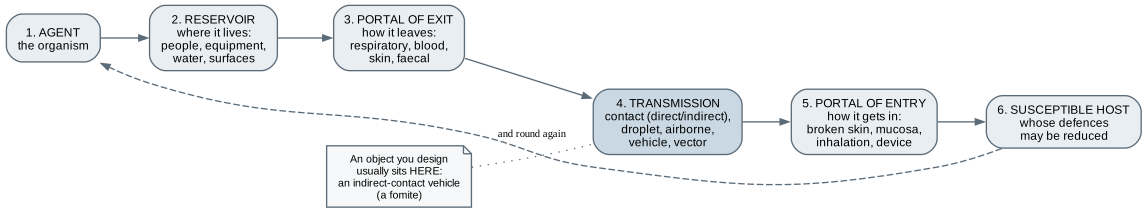
Your object is a fomite at the transmission link. Hand hygiene breaks the same link.
Not "does it touch a patient?" but "where does it go, who touches it, and what do they touch next?"
Cleaning, disinfection, sterilisation
Three different things
Three processes, in order
| Process | Definition | Typical methods |
|---|
| Cleaning | Physical removal of soil — the prerequisite for everything | Detergent, mechanical action, ultrasonic bath, washer |
| Disinfection | Inactivates many disease-causing organisms; not all spores | Alcohol, chlorine, quaternary ammonium, peroxide, heat |
| Sterilisation | Intended to eliminate all life, including spores; validated | Steam, ethylene oxide, hydrogen peroxide vapour, irradiation |
Cleaning must come first, always. A sterilisation cycle on a dirty instrument is not a sterilisation cycle.
Spaulding classification
| Category | Contact | Required processing |
|---|
| Critical | Sterile tissue or the vascular system | Sterilisation |
| Semi-critical | Mucous membranes or non-intact skin | At least high-level disinfection |
| Non-critical | Intact skin only | Low- or intermediate-level disinfection |
The category is set by the use, not the object. Your tabletop model is non-critical at most — say so in the brief.
Steam sterilisation — and what it destroys
Typical cycles
- Gravity: about 121 °C for 15–30 min
- Pre-vacuum: about 132–135 °C for 3–4 min
- Set and validated by the institution
Casualties
- PLA softens at 55–65 °C — a dishwasher deforms it
- PETG marginal; acrylic, many adhesives, elastic, electronics
- Survivors were chosen: 316 stainless, borosilicate, PEEK, many silicones
If a project needs steam sterilisation, that drives material and process selection from the beginning.
The finished object is the design
Whatever made it
A material claim is not device evidence
"Food safe", "medical grade", "biocompatible" — claims about a material as supplied. None is a claim about your finished object in your intended use.
Materials are evaluated in the context of a finished device and its intended use, not approved in the abstract.
What sits between the datasheet and the part
| Process | Hidden variables |
|---|
| Printing | Thermal history, additives, nozzle residue, layer voids, uncured resin |
| Machining | Coolant, burrs, embedded swarf, cross-contamination |
| Injection moulding | Release agent, regrind, parting lines, moulded-in stress |
| Casting | Mould release, cure inhibition, incomplete cure, bubbles |
| Sheet metal and welding | Heat tint, flux, free iron, lap-joint crevices |
| Glass | Residual stress, chips, seals to other materials |
| Textiles | Finishes, dyes, shrinkage, stitch holes, hook-and-loop |
| Electronics | Flux, coatings, adhesives, ingress around buttons and seams |
What actually varies from run to run
Additive manufacturing
- Orientation: weak between layers
- Infill: sealed voids until the shell breaks
- Same file, same printer, a month later — not identical
- Uncured resin is an irritant and sensitiser
Other methods
- CNC: tool wear, coolant; blind holes as bad as any cavity
- Moulding: a new resin lot or moulder is a new product
- Casting: under-cure is tacky and leaches
- Textiles: every wash changes dimension and strength
Each method has its own traceability record: file and profile, drawing and certificate, lot and cure log, pattern and batch, board and firmware.
Design for cleanability
- Every surface reachable by a gloved finger and a wipe
- Eliminate crevices, or make them openable without tools
- Radius internal corners; avoid exposed threads
- Continuous welds ground flush; passivate stainless
- Decide the soft-goods route: launder, wipe, or single use
- Seal the electronics; no fluid traps; labels that survive
Wood and fabric
Wood
- Porous and absorbent
- "Sealed" raises more questions than it answers
- Fine for demonstrations and fixtures in your own space
Fabric
- Everywhere in healthcare: slings, straps, sleeves, cushions
- Has its own route: laundering with thermal disinfection
- Every part must survive the wash — and still fit
Engineering bridge
Comparing candidate materials honestly
A material comparison — with the unknowns marked
| Material | Process | Autoclavable | Unresolved |
|---|
| PLA | Printing | No — softens 55–65 °C | Additives, porosity, machine history |
| Polypropylene | Moulding | Often, grade-dependent | Grade, release agent |
| Acrylic | Laser cut, machined | No | Crazes with alcohol wipes |
| Acetal | Machined, moulded | Limited | Steam degrades it over cycles |
| PEEK | Machined, moulded | Yes, repeatedly | Cost; coolant residues |
| 316L stainless | Machined, welded | Yes | Heat tint, passivation, crevices |
| Borosilicate glass | Glassblowing | Yes | Annealing; breakage is a sharps risk |
| Coated fabric | Sewn, welded seams | No | Coating cracks; stitch holes |
A comparison whose unknowns column is empty has not been done properly.
Devices, software, and training
Equipment and software
- Autoclaves, washer-disinfectors, low-temperature sterilisers
- Endoscope reprocessors — among the hardest problems
- UV-C systems: line of sight; eye and skin hazard
- Instrument tracking: which patients if a cycle fails?
Training
- Fluorescent marker under UV — the best single teaching tool
- Donning and doffing practice
- Cleanability coupons: printed, machined, cast, welded, sewn
The best first build — a UV hand-hygiene box
- Folded, powder-coated sheet metal or sealed laminate enclosure
- UV-A LEDs and driver; interlock and timer
- Wipeable gasket around the hand opening
- UV source shielded from the eyes — a hazard users cannot perceive
- State the objective first — "identify which areas you missed"
Worked example: the pivot cover
| Method | Strengths | Cleaning questions |
|---|
| Printed PETG shell | Fast to iterate | Layer lines, porosity, enclosed infill |
| Machined acetal halves | Smooth, tough, repeatable | Captive fasteners, deburring, coolant |
| Folded 316 sheet | Durable; survives anything | Edges, bend radii, weight |
| Cast silicone boot | No seams or fasteners | Cure; tears trap soil |
| Laser-cut acrylic | Transparent | Crazes with alcohol wipes |
First ask whether a cover is needed at all. Then choose the method. And a durability result is not a cleanliness result.
Workshop exercise and exit criteria
- Contact map: who touches what, and what they touch next
- Three materials by three methods — unknowns marked, no overall rank
- Redesign three hard-to-clean features
- Traceability record in the form that fits the method
- Cleanability coupons under UV: record what happened, not what you expected
What this chapter does not establish
- You cannot select a disinfectant or a sterilisation cycle
- You cannot declare any material safe
- You cannot validate a cleaning process
- A durability result is not a cleanliness result
- Biocompatibility testing is specialist territory
Next — Making it: choosing the technology and the method.